

There are many welding problems, but the most common of all is welding distortion. After hours of precise work to make sure everything is straight and in line, the final weld is completed.
But what happens when you discover that the component is warped, shrunken, twisted, and not straight at all?
A good understanding of welding distortion and its management is important, regardless of whether you are handling structural steel, pipelines, pressure vessels, or sheet-metal fabrication.
If you are able to control distortion, you can improve the quality of your weld, reduce waste of materials, and minimise rework requirements.
Welding Distortion prevention and management are the keys to better productivity. Let us break down everything you need to know about welding distortion.
What Is Distortion in Welding?
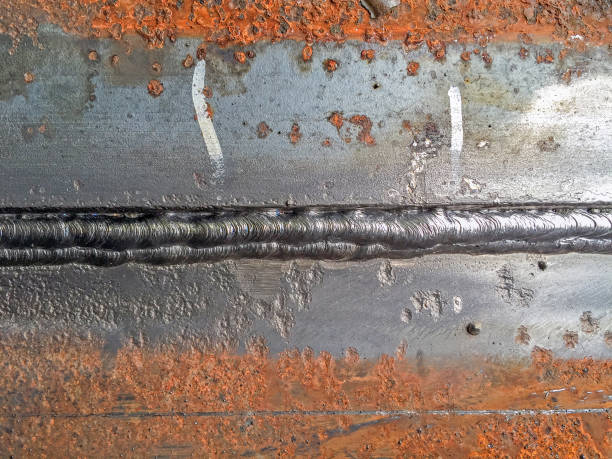
Welding distortion is when the shape, alignment, or dimension of a metal piece is altered due to heating and cooling during welding. This unwanted change occurs because metal expands when heated and contracts when cooled.
Welding focuses intense heat in a specific area of a metal piece, causing the expansion and contraction of that area to create uneven stresses. This internal stress can then permanently deform the metal.
To better understand the concept, let’s imagine you are welding two steel plates. The metal in the welding area will be heated while the rest of the metal will stay at a relatively low level of heat.
As the weld area cools, it begins to shrink. This shrinking created a pulling force, bringing the surrounding metal closer, which distorts the entire piece. So, distortion results from uneven welding shrinkage.
■Why Distortion Matters
You shouldn’t overlook distortion in welding because even minor distortions can cause serious damage. Let’s have a look at what issues distortion can cause:
- Bad dimensional accuracy
- Assembly misalignment
- Extra machining requirements
- Heavy fabrication costs
- Delay and reworks
- Diminished product quality
Welding distortion control is vital for industries that demand utmost precision, like aerospace, shipbuilding, and pressure vessel construction.
| Impact Area | Consequence |
|---|---|
| Dimensional Accuracy | Components fail to meet specifications |
| Assembly Fit-Up | Difficult or impossible assembly |
| Production Costs | Increased labor and material waste |
| Rework Time | Additional correction processes required |
| Product Quality | Reduced reliability and appearance |
| Project Schedule | Delays in fabrication and delivery |
Why Does Welding Distortion Occur?
You can’t avoid welding distortion without knowing what is causing it. So, here are some common causes of welding distortion.
Heat Expansion and Contraction
Thermal expansion and contraction are the main causes of distortion. Heating metal with a welding arc causes the heated area to expand. The cooler surrounding metal restricts expansion. Hence, internal stresses form.
After cooling begins, the weld metal contracts. The surrounding material resists this contraction. If the stresses exceed the yield strength of the material, then permanent deformation occurs.
Uneven Heating
If it were possible to heat and cool the entire structure uniformly, it is likely that there would be minimal distortion. However, welding focuses heat into a very small area.
For example, if you weld a long seam on one side of a plate, then the side that was heated shrinks more than the opposite side, causing an angular distortion.
Weld Metal Shrinkage
When metal cools and solidifies after welding, it will always shrink. You must know that the larger the volume, the larger the welding shrinkage force. This is why unnecessarily large welds create more distortion than smaller ones.
Restraint Conditions
How a component is clamped or supported in a particular place can also affect the distortion of a weld. If a component is free, it will move, which will cause distortion.
On the other hand, a firmly held component might be too heavily restrained despite appearing straight. In this case, the component can have a large amount of residual stress that can cause problems later.
| Cause | How It Creates Distortion |
|---|---|
| Heat Expansion & Contraction | Creates internal stresses during cooling |
| Uneven Heating | Causes one area to shrink more than another |
| Weld Metal Shrinkage | Pulls surrounding material inward |
| Restraint Conditions | Restricts movement and generates residual stress |
| Excessive Heat Input | Enlarges heat-affected zone and shrinkage forces |
Types of Distortion in Welding
Different welding situations can result in different types of distortions. Knowing the patterns and types of distortion in welding can help you identify problems and correct them in a timely manner.
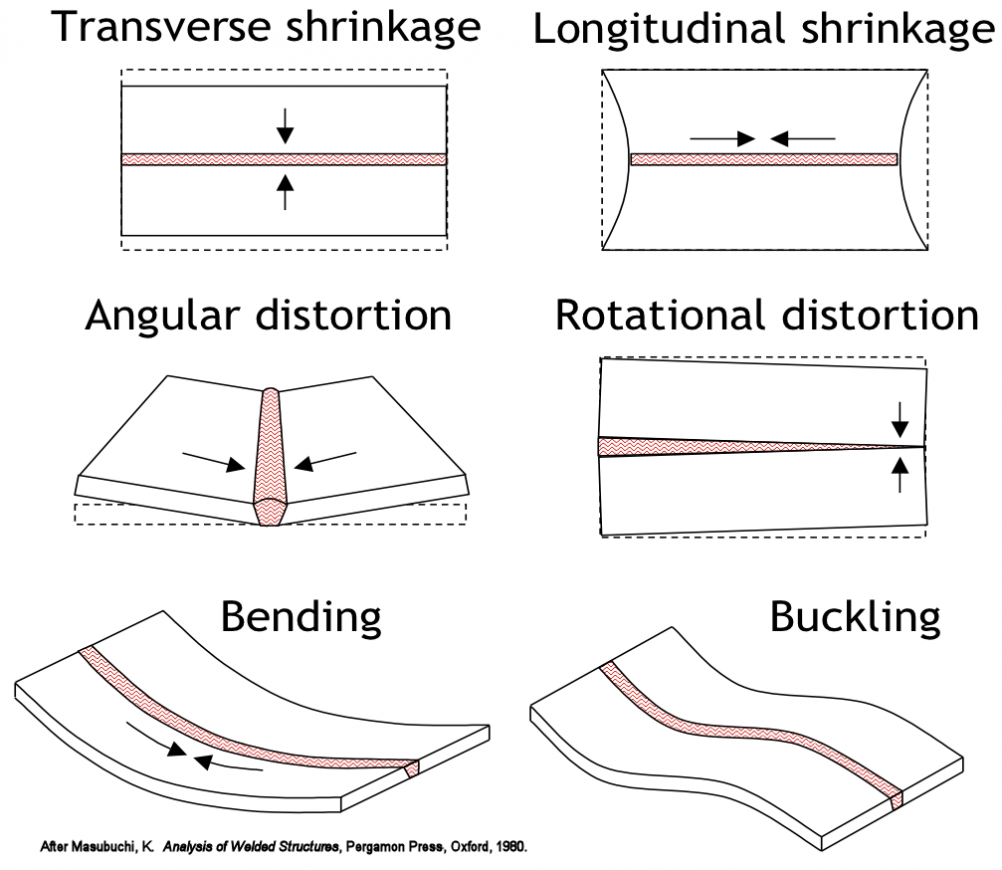
1. Longitudinal Shrinkage
Longitudinal shrinkage refers to welding shrinkage that occurs parallel to the direction of the weld. It runs along the length of the weld. So, when the weld begins to cool, it contracts. This contraction generates a force that shortens the component in the same direction as the weld bead.
Suppose, you have to weld a steel beam of 3 meters along its length. It is reasonable to expect that after the weld cools, the beam would pull the material in an inward direction of the weld. Hence, the beam would be slightly shorter after the weld cools.
Characteristics:
- Parallel shrinkage to the direction of the weld
- Most noticeable for long weld seams
- Most shrinkage will occur in the overall component dimension.
2. Transverse Shrinkage
Transverse shrinkage refers to shrinkage that occurs perpendicular to the weld. It runs across the weld. A weld that is cooling will pull each side of the joint toward the center of the weld.
Suppose, you have to weld two steel plates of width 0.5 meters and length 1 meter together with a butt joint. After the weld cools, the plates would have moved closer together. This will result in a reduced overall width.
Characteristics
- Occurs perpendicular to the direction of the weld
- Very noticeable in butt joints
- Results in a reduction in width
3. Angular Distortion
Angular distortion in welding occurs when shrinkage is uneven across material thickness. This welding deformation frequently occurs when one side of the joint has more welded metal than the other. The welded metal that has more volume will shrink more and pull the plates into an angular position.
A single-V groove weld is a prime example of angular distortion in welding. The top side has more volume of weld metal than the bottom side.
Characteristics
- The volume of material on one side shrinks more than the other.
- An angular change is noticeable.
- Commonly seen in fillet and groove welds.
4.Bowing Distortion
Bowing distortion occurs when a welded component bends along its length. This distortion occurs when the weld is placed away from the component’s neutral axis. For example, a long rectangular frame welded on one side only will curve to form a bow-like shape after cooling.
Characteristics
- Creates a structure that is curved
- Common in welded frames and beams
- Results from shrinkage that is not balanced
5. Buckling Distortion
Buckling distorts thin sheets of metal. Buckling distortion happens when compressive stress is generated during the welding process, which exceeds the stiffness of the metal. This causes the thin metal sheet to ripple, wave, or buckle. An example of buckling welding deformation occurs when you weld thin sheets of stainless steel. It causes the ‘oil-canning’ effect in which the sheet will form visible ripples.
Characteristics
- Usually happens in thin materials.
- Creates ripples or waviness
- Difficult to rectify the distortion, especially when the distortion is severe.
6. Twisting Distortion
Twisting distortion happens when different parts of the welded structure shrink unevenly. As a result, uneven twisting of the structure occurs, known as rotational distortion. For example, after you weld multiple corners of a fabricated box section, it might twist slightly along its length.
Characteristics
- Creates spiral deformation
- Mostly seen in complex fabrication.
- Occurrence due to uneven welding sequencing
| Distortion Type | Direction | Common Appearance | Typical Applications Affected |
|---|---|---|---|
| Longitudinal Shrinkage | Along weld length | Shortening of component | Beams, long seams |
| Transverse Shrinkage | Across weld | Reduced width | Butt joints |
| Angular Distortion | Through thickness | Plates rotate or angle | Fillet and groove welds |
| Bowing Distortion | Along structure length | Curved profile | Frames, beams |
| Buckling Distortion | Surface deformation | Ripples or waves | Thin sheet metal |
| Twisting Distortion | Rotational | Spiral-like deformation | Box sections, complex fabrications |
Factors Affecting Welding Distortion
There are various factors that affect the amount of welding distortion you might end up with. Let’s have a look at which factors you must consider when welding.
● Heat Input
Heat input is one of the most strongly related factors affecting welding distortion.
More heat input factors mean:
- Larger heat-affected zones
- More expanding
- More contracting
- Greater welding deformation risk
For example, slow welding speed and high amperage produce much more distortion compared to a faster welding speed and a low amperage.
● Material Properties
Different metals behave differently when subjected to welding heat. The greater the coefficient of thermal expansion of a material, the more distortion is likely to occur. Compared to carbon steel, stainless steel, and aluminum are much more likely to experience distortion.
● Plate Thickness
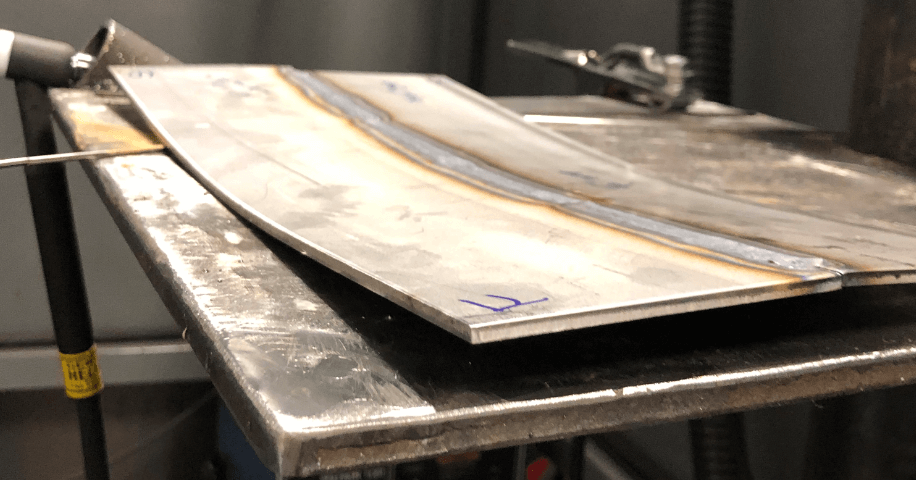
Thin materials are easily distorted due to their low resistance to shrinkage forces. For example, a 2 mm metal sheet can be significantly distorted. On the other hand, a 25 mm metal plate may show only a few signs of distortion.
● Joint Design
Weld volume and shrinkage are directly influenced by the shape of a joint. If you have a poor joint design, it can increase the chances of distortion. Bad joint designs can be those that have large groove angles, excessive root openings, or fillet welds that are too large. So, it’s better to have a balanced joint design to reduce the chances of distortion.
● Welding Sequence
The sequence in which the welds are applied affects the distribution of stresses. If the sequence is improper, the forces that cause shrinkage may be concentrated, and the chances of distortion may be increased. Balanced welding sequences often help distribute the stresses more evenly.
● Restraint and Fixturing
To maintain the position of components that are being welded, various clamps, jigs, fixtures, and strongbacks may be used. These help minimise the movement of components during the welding process.
However, you must remember that too much restraint may lead to an increase in residual stresses. The ideal situation is having the appropriate amount of restraint that minimizes movement but also doesn’t contribute to residual stresses.
| Factor | Low Distortion Risk | High Distortion Risk |
|---|---|---|
| Heat Input | Low amperage, faster travel speed | High amperage, slower travel speed |
| Material Type | Carbon steel | Stainless steel, aluminum |
| Plate Thickness | Thick plates | Thin sheets |
| Joint Design | Balanced joints | Large groove angles, oversized welds |
| Welding Sequence | Balanced sequence | Continuous one-sided welding |
| Restraint | Proper fixturing | Too little or excessive restraint |
How to Prevent Distortion in Welding
Although you can correct the distortion, it is less effective and more expensive than avoiding distortion altogether.
1. Minimize Heat Input
Your goal must be to use as little heat as possible and still achieve satisfactory fusion. This can be accomplished if you select a higher travel speed. You can even reduce the weld size or choose a more favourable welding process. It is also recommended to eliminate unnecessary weld passes. By adding less heat, you can lower the chances of distortion.
2. Use Proper Joint Design
Weld volume can be reduced through good joint design. Some examples include double-V groove joints rather than opting for single-V groove joints. You can select smaller groove angles and even optimise root openings. By choosing a balanced design, you can reduce the forces that cause shrinkage.
3. Apply Balanced Welding
It is best to place welds in a balanced manner. You must ensure the symmetry. For instance, if you weld one side of a structure, make sure you weld on the opposite side as well. If you balance the shrinkage, you can maintain good alignment.
4. Use Skip Welding
In skip welding, welds are placed in segments in many different scattered locations. They aren’t placed continuously from one end to the other. The advantages of skip welding include less heat concentration, decreased distortion, and improved stress distribution.
5. Use Back-Step Welding
In back-step welding, short welds are placed in the opposite direction of the overall welding. This helps to control shrinkage and improve the overall dimensional control in the welded structure.
6. Use Clamps and Fixtures
Good fixturing aids in the prevention of excessive movement during the welding process. Common tools used include tack welds, jigs, strongbacks, and clamps. These tools maintain the proper alignment during the welding process.
7. Presetting
This technique purposely places parts opposite to the expected distortion. As the weld cools down and shrinks, the parts move into the desired final location. An example of this technique can include, if a weld is expected to bend up by 3 degrees, it should be bent down by the same angle before welding is done.
| Prevention Method | How It Helps |
|---|---|
| Minimize Heat Input | Reduces thermal expansion and shrinkage |
| Proper Joint Design | Lowers weld volume and shrinkage forces |
| Balanced Welding | Equalizes shrinkage forces |
| Skip Welding | Prevents heat concentration |
| Back-Step Welding | Controls contraction stresses |
| Clamps and Fixtures | Maintains alignment |
| Presetting | Compensates for expected distortion |
How to Correct Welding Distortion
What happens when you end up with welding distortion? Here are some effective strategies to help you correct these distortions in order to improve the accuracy of the dimensions.
● Mechanical Straightening
Mechanical straightening is a technique that involves the application of physical force. The force helps return the components to their desired shape.
For mechanical straightening, you can use pressing, rolling, jacking, and hammering. This technique is most effective when the distortion is just a little bit.
● Thermal Straightening
Thermal straightening involves the application of heat, which creates a shrinkage force opposite to the distortion. The area that is heated expands, and then when it is cooled, it contracts.
The contraction pulls the component back into alignment. This method is often utilised in shipbuilding and in the fabrication of structures.
● Flame Straightening
Flame straightening is a form of specialized thermal correction method. In this case, a torch applies controlled heat in a predetermined pattern on selected areas. When the metal is cooled, it shrinks to correct the distortion by itself.
● Stress Relief Heat Treatment
Stress relief heat treatment is a method that minimises the residual stresses. It is done by evenly heating the entire metal to a predetermined temperature, followed by gradual cooling.
The benefits include a reduction in residual stress in welding, improvement in the stability of dimensions, and a reduction in the likelihood of cracks.
● Controlled Re-Welding
Distortion can be addressed using strategically positioned corrective welds. For example, you can apply a weld on the opposite side of a distorted component where shrinkage has occurred. This will create a shrinkage force pulling the structure back into the desired position.
● Using Advanced Welding Equipment
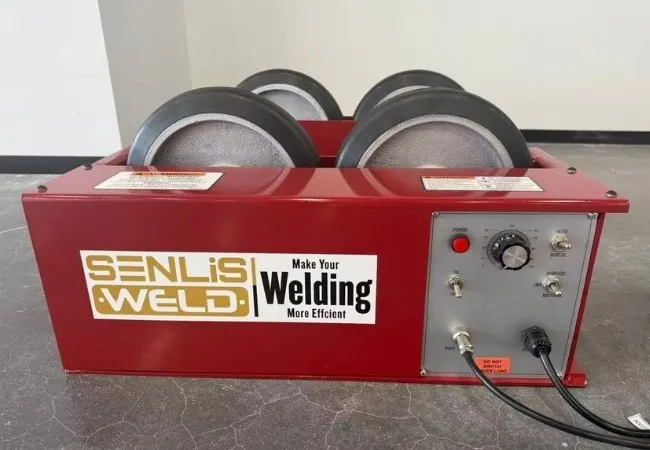
Today, advanced welding equipment allows better control over heat and improved precision. This has greatly reduced welding distortion.
SENLISWELD, for example, is one of the manufacturers that has a sophisticated welding product line.They have advanced welding solutions that offer better control of heat input, improved weld quality, and lower distortion.
By implementing the correct equipment and technology, you can greatly minimize the need for post-welding corrective work.
| Correction Method | Principle | Best Used For |
|---|---|---|
| Mechanical Straightening | Physical force | Minor distortion |
| Thermal Straightening | Controlled heating and cooling | Moderate distortion |
| Flame Straightening | Localized torch heating | Structural fabrication |
| Stress Relief Heat Treatment | Removes residual stress | Pressure vessels, heavy fabrications |
| Controlled Re-Welding | Counteracts shrinkage | Specific localized distortion |
| Advanced Welding Equipment | Precise heat input control and automated welding parameters | Reducing distortion during fabrication and minimizing corrective work |
Conclusion
Distortion in welding is a common problem often seen when there is uneven heating, cooling, and weld shrinkage. There are many ways to correct the problem, but it’s better to prevent it altogether.
You can save your weld from distortion by properly planning the process, selecting a good joint design, managing heat carefully, implementing the right weld sequence, and using effective fixturing.
Even if you fail to prevent it, you must understand the different types of distortion. It will help you identify them easily and repair them before they become costly.
These preventative and corrective techniques work side by side to help you improve dimensional accuracy, reduce rework, and lowers the residual stress in welding.
By welding distortion control, you can produce higher-quality welded components consistently.
Frequently Asked Questions
1. What causes distortion in welding?
A: Distortion happens because of the expansion and contraction of the welded metal. The distortion depends on the localized heating that eventually will make parts shrink unevenly. This introduces several internal stresses that will cause the workpiece to bend and twist, or even warp.
2. What is angular distortion in welding?
A: Angular distortion in welded joints occurs when one side contracts more than the other during the cooling process. This causes unequal shrinkage that will cause the plates to rotate and affect the alignment of the welded joint.
3. How can you reduce welding distortion?
A: You can minimize the amount of distortion experienced by using less heat input and consistent welds, along with appropriate fixturing and joint designs. Additionally, applying skip welding and an appropriate welding sequence can help reduce distortion.
4. What is residual stress in welding?
A: Residual stress refers to stress that is “locked in” or sealed in a welded component after it has cooled. Restrained weld shrinkage leads to residual stress. This type of stress can affect the performance of the structure, the stability of the dimensions, and the overall life of the structure.
5. Can welding distortion be corrected?
A: Yes. Welding distortion can be fixed through the application of mechanical straightening methods, or can be fixed through flame or thermal straightening. Stress relief heat treatment or controlled corrective welding can also be used to fix distortion, depending on the severity of the distortion that has taken place.
Recommend Reading
Types of Welding Joints – SENLISWELD
14 Common Welding Defects Causes and Remedies – SENLISWELD
Welding Tips and Tricks – SENLISWELD
Porosity in Welding – SENLISWELD


 EN
 ES
 RU
 JA
 FR
 PT